



GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Explore our primary manufacturing catalog engineered for professional clubs, corporate athletic brands, and enterprise teamwear distributors globally.
Analyzing the shift from commoditized luggage to specialized, high-tenacity equipment carrying systems in the global athletic and enterprise procurement sector.
Historical procurement models prioritized baseline unit costs at the expense of structural longevity and ergonomic distribution. Contemporary supply chain analysis demonstrates that shifting toward high-tenacity TPU-coated fabrics, automated bar-tack reinforcement, and vertically integrated OEM/ODM manufacturing reduces total cost of ownership (TCO) by up to 34% over a three-year team gear lifecycle.
From smart storage architecture to sustainable polymer substrates, technical requirements are redefining how equipment bags are manufactured.
Transition from basic 600D polyester to 1680D Ballistic Nylon and Thermoplastic Polyurethane (TPU) laminated membranes, delivering complete water impermeability, puncture resistance, and extreme tear strength under heavy loading conditions.
Integration of silver-ion antimicrobial linings to prevent bacterial odor buildup, alongside expandable wet/dry shoe compartments, internal padded laptop sleeves, and removable gear dividers designed for multisport flexibility.
High-resolution digital dye-sublimated panel printing, laser-engraved hardware, and integrated RFID asset tracking tags allowing clubs to effortlessly manage gear checkout, inventory auditing, and individual athlete identification.
How enterprise buyers evaluate direct-from-factory partnerships to balance volume pricing, brand consistency, and long-term durability standards.
| Evaluation Parameter | Standard Commercial Grade | GoldenLeaf OEM Industrial Grade | Procurement Advantage |
|---|---|---|---|
| Primary Shell Material | 400D Polyester / Thin PVC Film | 1680D Ballistic Nylon / TPU Matte Membrane | +300% Tensile Strength & Abrasion Resistance |
| Zipper Hardware | Standard #5 Nylon Coil Zippers | Heavy-Duty YKK #10 Waterproof Sealed Zippers | Eliminates Zipper Burst Under Maximum Capacity |
| Stitching & Load Points | Single-Needle Stitching (8 Stitch/Inch) | Dual-Needle Automated Bar-Tack (14 Stitch/Inch) | Supports Dynamic Load up to 45 kg (100 lbs) |
| Color Fastness Standard | Grade 2.5 - 3.0 (Fades after UV exposure) | Grade 4.5+ Sublimation Ink (ISO 105-B02 Tested) | Vibrant, Fade-Resistant Team Colors Year-Round |
| Customization Versatility | Limited Screen Printing (Prone to Peeling) | Full Edge-to-Edge Sublimation + Woven Badges | Unrestricted Pantone Matching & Player Personalization |
Inside GoldenLeaf Sports' 3,000 m² Shenzhen facility—where automated digital workflow meets decade-tested artisanal tailoring.
Established in 2011 in Longgang District, Shenzhen, GoldenLeaf Sports (ShenZhen) Co., Ltd. operates at the center of the world's most sophisticated apparel and hardware manufacturing cluster. By housing automated computer-guided laser cutting, RIP color-management dye sublimation printing, structural assembly, and multi-stage quality control under one roof, we eliminate intermediate supply chain friction.
With over 160 skilled technicians—80% holding over 8 years of specialized equipment manufacturing experience—our facility delivers agile lead times, shipping 300 to 1,000 customized team units within 12–18 working days post-approval.
Quality control is embedded directly into our automated line operations. A dedicated 5-person QA inspection team audits raw fabric tensile strength, zipper fatigue resistance, and print color matching using spectrophotometric analysis prior to cutting.
"Low Minimum Order Quantity (MOQ) Flexibility: 10 pieces per design, allowing personalized name, squad number, and sponsor logo variations within a single production batch at zero setup surcharge."
Tailored engineering configurations optimized for specific sport demands, enterprise events, and commercial markets.
High-capacity equipment bags for Lacrosse, Rugby, Hockey, and American Football engineered with reinforced structural bases, padded stick/helmet straps, and ventilated moisture evacuation zones.
Durable student-athlete backpacks and travel duffels featuring personalized player numbers, ergonomic dual-density shoulder straps, and heavy-duty wear-resistant bottom panels.
Premium executive travel gym bags, weekend duffels, and branded event carry-ons created for promotional merchandise distributors and corporate team-building events.
Heavy-duty transport gear equipped with MOLLE webbing systems, weatherproof storm flaps, and ultra-durable zippers tailored for extreme outdoor, fishing, and expedition use.
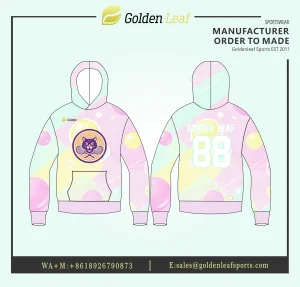
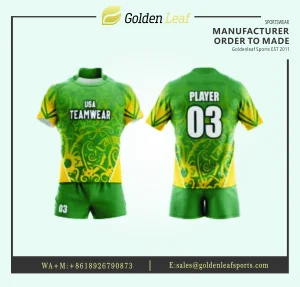
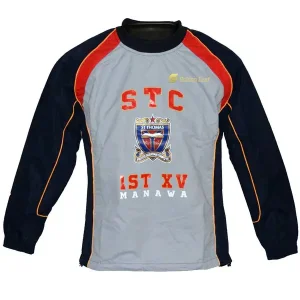
Discover our wide array of customizable sports apparel, outerwear, and accessories manufactured with identical high-tenacity standards.
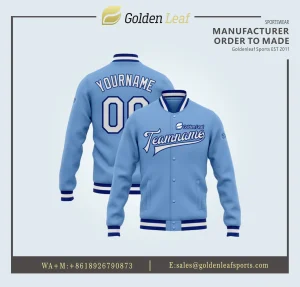
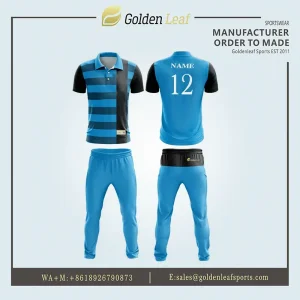
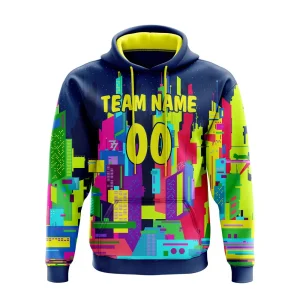
Ensure your chosen manufacturing partner satisfies critical quality, compliance, and capacity requirements before issuing RFQs.
Verify that raw substrates undergo hydrostatic head testing for waterproofing, Martindale abrasion resistance testing (>50,000 cycles), and ISO color fastness validation.
Confirm the factory utilizes high-density polyester thread (T-70 or higher), computerized multi-pass bar-tacking on all webbing joints, and taped waterproof seams where applicable.
Choose partners capable of returning 24–48 hour digital 3D artwork renders and physical pre-production samples within 5–7 working days to accelerate market delivery.
Detailed responses from our engineering and export team addressing common procurement, technical, and logistic queries.
Our baseline flexible MOQ starts at just 10 pieces per design for custom sublimated team jerseys, gear bags, and equipment pinnies. Because every item is cut and printed on demand, individual player names, squad numbers, and specific size gradations (from Youth 6Y to Adult 5XL) can be mixed within the same 10-piece order at no extra charge. Custom knitted items such as technical socks or structured caps carry separate minimums based on machine setup.
We utilize imported eco-friendly sublimation inks combined with advanced RIP color-management software calibrated to Pantone Matching System (PMS) standards. Before mass production, our technicians perform sample strike-offs on actual production fabric panels, verifying color fastness (Grade 4.5+) and tone consistency under standardized D65 lighting environments.
Digital vector mock-ups are delivered within 24 to 48 hours of artwork submission. Physical pre-production samples require 5 to 7 working days. Bulk manufacturing of 300 to 1,000 units is completed within 12 to 18 working days inside our 3,000 m² Shenzhen plant. Global express air freight typically takes an additional 4 to 7 business days depending on destination.
Yes, full Original Design Manufacturing (ODM) and private-label services are available. We manufacture custom heat-transfer inner neck labels, woven side seam tags, branded hangtags, barcode stickers, printed polybags, and custom master cartons tailored to your brand's specific retail or distribution requirements.
We support standard global shipping terms including EXW, FOB Shenzhen/Yantian, CIF, and DDP (Delivered Duty Paid) via express couriers (DHL/FedEx/UPS), air cargo, or ocean freight. We offer secure T/T bank transfer, Wire, and major credit options with full pre-dispatch photographic quality control reports provided.