GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
GoldenLeaf Sports14+ Years Teamwear Manufacturer · Shenzhen, China
Engineered with micro-mesh ventilation, digital dye-sublimation, and high-tenacity polyester blends.
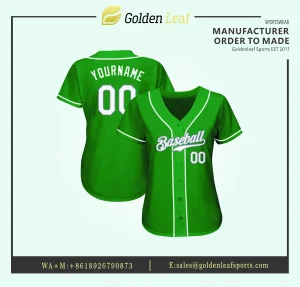
An authoritative analysis of global procurement trends, material science innovation, and supply chain agility in custom athletic apparel.
The global sportswear and active outerwear market is undergoing a structural paradigm shift. Once categorized merely as pre-game warm-up gear, the modern U-Tracksuit and technical athletic jacket have transformed into high-performance, multi-functional apparel items required by professional sports clubs, academic institutions, fitness franchises, and retail brands worldwide. As user search intent shifts from generic sourcing queries toward specific technical requirements—such as moisture-wicking indices, thermal regulation, dye-sublimation colorfastness, and eco-certified supply chains—manufacturers must elevate their technical transparency and execution precision.
Key Market Insight: Semantic search analytics reveal that B2B procurement managers no longer search exclusively for "cheap tracksuit factory." Sourcing intent is heavily skewed toward high information gain parameters: custom pattern grading, low MOQ flexibility (10-50 pcs/run), zero color-bleeding guarantees, and direct-to-factory OEM/ODM integrated capabilities in major textile hubs like Shenzhen.
Expanding athletic leagues across North America, Europe, and Oceania drive sustained demand for sublimated team warm-up suits, lightweight windbreakers, and heavy-duty bomber jackets.
Transition from basic cotton-poly blends to high-tech 100% polyester interlock (145–280 GSM), 4-way stretch poly-spandex (88/12), and breathable micro-mesh lining engineered for modern athletes.
Direct factory execution eliminates agent Markups. Quality control integrated at panel cutting, RIP color sublimation, and twin-needle seam assembly ensures zero-defect delivery.
Leveraging Guangdong's complete textile supply chain, advanced digital printing tech, and master garment craftspeople.
Situated in the heart of the Pearl River Delta apparel cluster, our manufacturing operations benefit from immediate access to world-class yarn spinners, specialized dye houses, and technical trim suppliers. Whether your project demands ultra-lightweight windbreaker shells, fleece-lined cold-weather track pants, or custom elastic jacquard waistbands, raw material turnaround times are reduced by up to 60% compared to alternative Asian markets.
Traditional screen printing layers ink on top of fabric, causing stiffness, poor breathability, and eventual cracking or peeling after washing. Our Shenzhen facility utilizes high-precision digital sublimation plotters loaded with imported, eco-friendly sublimation inks. Under controlled thermal pressure (200°C+), gaseous dye penetrates deep into the polyester polymer matrix, producing rich Pantone-matched colors with Grade 4+ wash fastness without restricting skin airflow.
To eliminate manual misalignment during garment assembly, printed fabric sheets pass directly to automated optical laser cutting machines. Laser optics read camera registration marks printed alongside your graphics, cutting each jacket body, sleeve, collar, and pocket panel with sub-millimeter accuracy. This ensures that multi-panel side stripes, sponsor graphics, and complex aboriginal or geometrical patterns align seamlessly across seams.
We solve the common buyer dilemma of rigid factory minimums. By digitizing our pattern master library, we efficiently handle orders ranging from a 10-piece custom club roster run with distinct player names/numbers to high-volume 100,000-piece seasonal apparel drops for global distributors, maintaining strict visual and dimensional consistency across every unit.
Comprehensive technical metrics engineered for athletic performance, institutional durability, and extreme climate adaptability.
| Garment / Product Type | Primary Fabric Composition | Weight (GSM) | Key Performance Features | Optimal Application Scenarios |
|---|---|---|---|---|
| Pro-Performance U-Tracksuit | 100% Poly Interlock / Poly-Spandex Blend | 220 - 280 GSM | Moisture Wicking, 4-Way Stretch, Brushed Fleece Interior Option | Professional Club Warm-Ups, Sideline Staff, National Teams |
| Lightweight Athletic Windbreaker | 100% Micro-Ripstop Polyester with DWR Coating | 90 - 130 GSM | Water Repellent, Windproof, Packable, Underarm Ventilation Mesh | Outdoor Running, Track & Field, Marathon Event Merch |
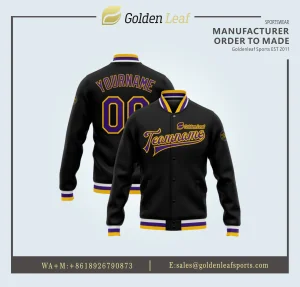
| Varsity & Baseball Bomber Jacket | Heavy Duty Poly-Twill Shell / Satin Lining | 300 - 380 GSM | Ribbed Collar & Cuffs, Reinforced Snap Buttons, Thermal Insulation | School Athletics, University Merch, Lifestyle Streetwear Brands |
| Sublimated All-Weather Training Jacket | 3-Layer Laminated Softshell (TPU Membrane) | 260 - 320 GSM | 10,000mm Water Column Protection, Breathable Membrane, Fleece Backing | Winter Sport Training, Coaching Staff, Alpine & Outdoor Sports |
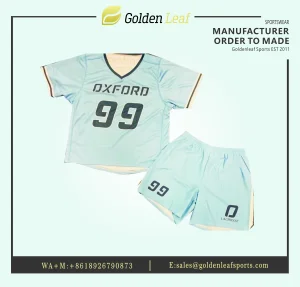
| Reversible Squad Practice Track Top | Dual-Layer Lightweight Bird-Eye Micro Mesh | 145 - 160 GSM | Dual-Color Outer/Inner Sublimation, Zero Color Bleed, Quick Dry | Basketball / Lacrosse Squad Scrimmages, Youth Sports Leagues |
From high-impact school sports leagues to corporate identity apparel and high-end private label fashion.
Sports organizations require unified aesthetic identities across travel suits, warmup jackets, and bench coats. Our sublimation process allows every athlete to have their personalized name, squad number, and sponsor configuration printed crisp without additional setup fees per panel.
Multinational corporations, security personnel, and promotional event operators order custom jackets for brand visibility. We provide custom embroidery, high-density silicone heat-transfer logos, woven neck labels, and branded zipper pulls to reinforce corporate brand prestige.
Emerging streetwear and athletic fashion brands demand fast design-to-market pipelines. We offer end-to-end ODM assistance—from digital tech pack creation and physical pre-production prototyping in 5–7 days to customized polybag packaging ready for direct fulfillment.
Operating under rigorous quality control standards since 2011 to deliver world-class athletic wear globally.
GoldenLeaf Sports (ShenZhen) Co., Ltd. brings together all critical production stages under a single roof in Longgang District, Shenzhen. Our workforce of over 160 skilled technicians—80% of whom hold senior garment manufacturing credentials—manages design vectorization, printing paper transfer, fabric lamination, laser cut panels, and flatlock assembly.
By eliminating third-party sub-contracting for printing or sewing, we guarantee strict control over production timelines, fabric shade consistency, and seam stress tolerances across every production batch.
Our five full-time QA/QC inspectors execute comprehensive inspections across five key stages:
In-depth technical answers regarding minimum order requirements, fabric customization, shipping terms, and ODM private labeling.
Built for rigorous athletic performance, outdoor training, and club branding.
Partner with Shenzhen's leading OEM/ODM teamwear manufacturer. Request a factory-direct quote, virtual mockup, or physical fabric swatch book today.